Fire Pipe Drilling Machines for Fire Protection and Grooved Pipe Systems
As a Engineering Construction Pipeline Connection Solutions manufacturer, we match product configuration to the application, operating limits, interfaces and acceptance criteria defined for each project.
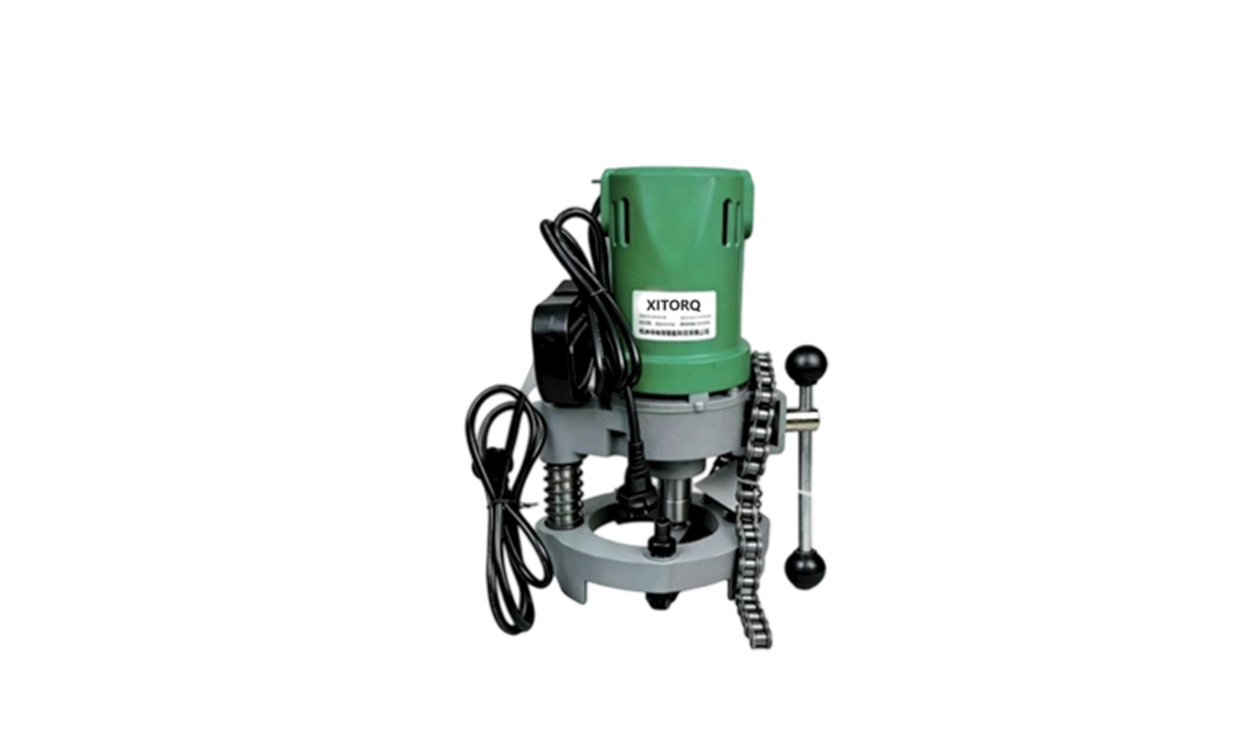
Hangzhou Xinabo Intelligent Electromechanical Technology Co., Ltd designs and builds pipeline connection equipment for fire protection engineering, building services and industrial pipework. Our Fire Pipe Drilling Machine manufacturer range covers the branch-outlet and coupling-preparation stage of a grooved or threaded system, producing clean, correctly positioned holes before the joint is assembled.
Established in 2010, we have developed nine generations of intelligent pipe processing machines, supported by 30 patents and National High-tech Enterprise recognition. Fire protection contractors, MEP installers and pipeline construction companies use our equipment to move hole cutting off the site bench and into a repeatable, fixture-controlled operation.
Working envelope: 220V industrial drive, φ16–φ114 mm hole capacity, DN15–DN200 pipe compatibility, mechanical clamping fixture for hole positioning, and built-in overload protection that stops the tool on hard pipe walls.
Our Pipeline Connection Range and Where Each Machine Fits
Hole cutting is one step in a sequence. We supply the surrounding stages as well, so a project can be equipped from pipe pre-treatment through to pressure acceptance with machines that share the same working logic and service support.
| Equipment |
Function in the connection sequence |
Typical application |
| Fire Pipe Drilling Machine |
Hole cutting for branch outlets, grooved couplings and sprinkler take-offs |
Fire mains and sprinkler piping in galvanized and seamless steel, DN15–DN200 |
| Intelligent Threading Machine |
Automatic pipe diameter recognition and thread cutting, DN15–DN100 |
Threaded risers and distribution pipe in carbon steel, galvanized, stainless, aluminium and copper |
| Intelligent Pipe Tightening Machine |
Electric screwing with adjustable torque and automatic return |
Assembling threaded joints in the fabrication shop or on site |
| Variable Frequency Cold Saw |
Burr-free cold cutting to length |
Pipe pre-treatment ahead of threading, drilling or grooving |
| Electric Pressure Test Pump |
Hydrostatic testing of completed pipework |
Handover and acceptance testing |
| Oil-Free Piston Air Compressor |
Clean, oil-free compressed air supply |
Pneumatic tooling and air-assisted operations |
| Cordless Power Tools and Precision Threading Dies |
Battery-powered cutting, punching, drilling and fastening; cutting dies and consumables |
Overhead and remote work, plus thread quality maintenance |
Hole Capacity, Pipe Range and Working Specifications
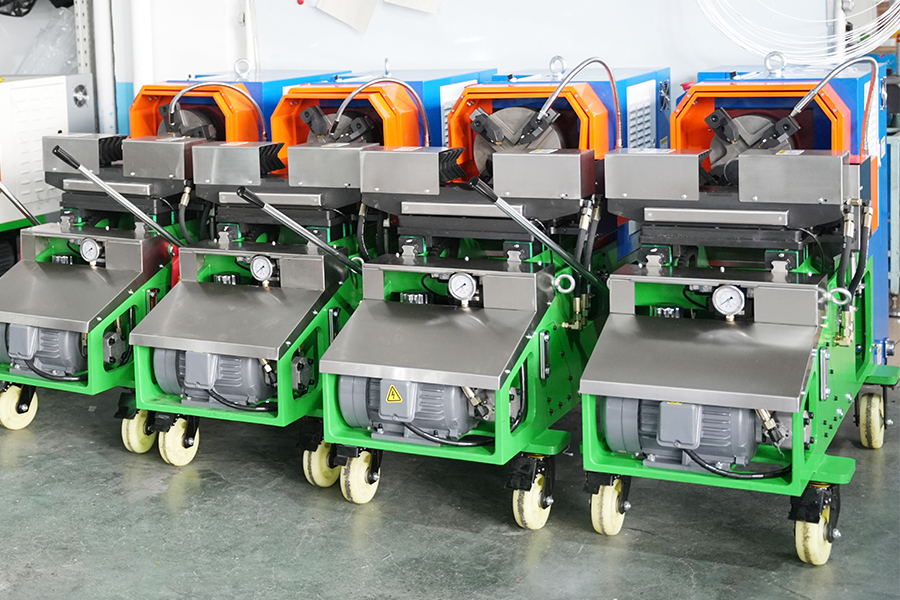
The machine is built around a 220V industrial motor and a high-precision cutter head. It produces standard-sized holes with smooth, burr-free edges, so the outlet or coupling seat does not need a second finishing pass before assembly.
| Parameter |
Specification |
| Drive |
220V industrial motor |
| Hole diameter range |
φ16–φ114 mm |
| Compatible pipe sizes |
DN15–DN200 |
| Pipe materials |
Galvanized steel pipe, seamless steel pipe, PVC pipe, carbon steel, stainless steel, aluminium, copper |
| Hole edge condition |
Smooth and burr-free; no secondary finishing required |
| Positioning |
Pipe clamping fixture for accurate hole location across pipe diameters |
| Safety |
Built-in overload protection with automatic stop on hard pipe walls |
Application Fit in Fire Protection and Building Services
Fire protection work sets the requirements: pipe runs are long, diameters change frequently, and every outlet has to line up with the branch line it feeds. A fixture-clamped drilling operation keeps hole centrelines consistent along the run and removes the variation that comes from freehand drilling.
- Sprinkler and standpipe mains — branch outlets cut into DN50–DN200 steel mains before grooved couplings or welded bosses are fitted.
- Grooved pipe system fabrication — outlet holes prepared to the coupling diameter before the housing and gasket are assembled.
- Galvanized pipework — clean cutting that limits coating damage around the hole edge.
- Plumbing and MEP installation — take-offs on risers, plant-room headers and distribution pipe.
- Prefabrication shops — repeatable hole patterns on spool pieces before delivery to site.
Configuration Options and Tooling
We configure each machine against the pipe schedule and hole sizes on the project drawings rather than a single default specification.
- Cutter head and bit sizes matched to the outlet diameters used in the system, within the φ16–φ114 mm range.
- Clamping fixture sized for the pipe diameter band being processed, so the pipe is held without rotation or slippage during cutting.
- Voltage and plug configuration for the destination market and site supply.
- Spare cutter heads and consumables supplied with the machine for continuous production.
Controls, Safety and Integration with the Fabrication Line
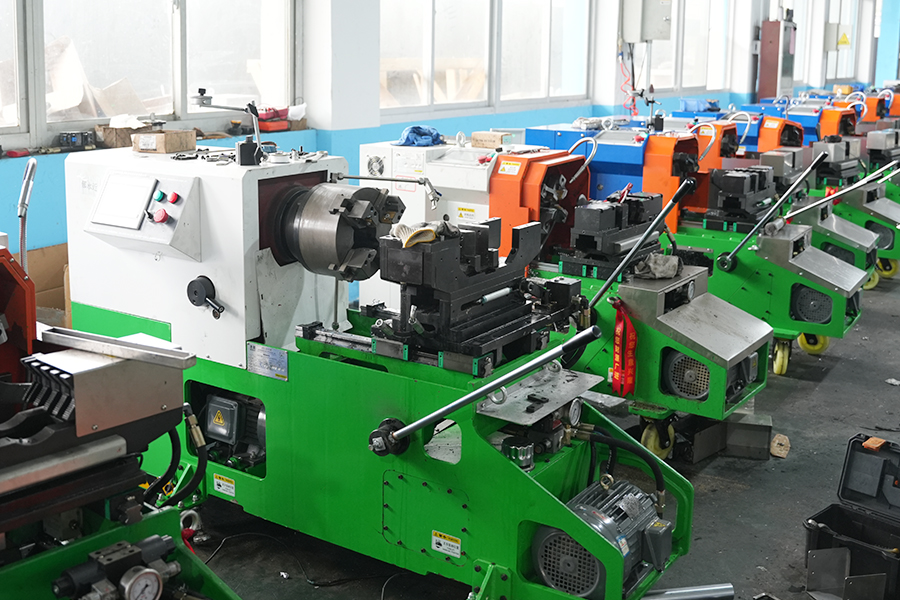
The machine runs from a single operator position. The pipe is clamped, the cutter is aligned to the marked centreline, and feed is applied through the machine rather than by hand pressure. Overload protection monitors cutter load and stops the tool when it meets a hard section of pipe wall, protecting both the operator and the cutter head.
In a fabrication shop the drilling machine sits between the cold saw and the threading or grooving station. Because the clamping fixture references the pipe outside diameter, hole positions can be marked from a common datum along the spool, keeping the sequence consistent when several operators work on the same run.
Quality Control, Conformity and Acceptance
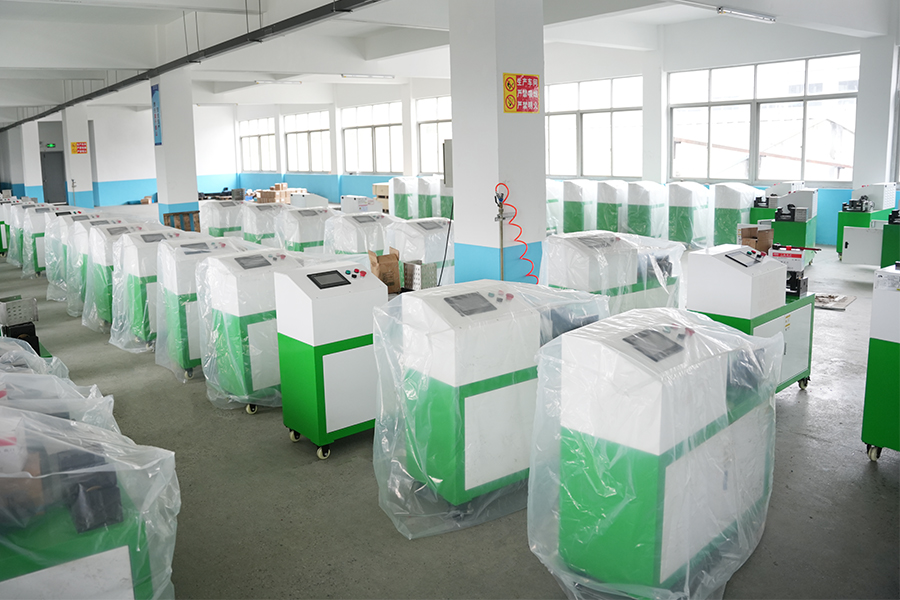
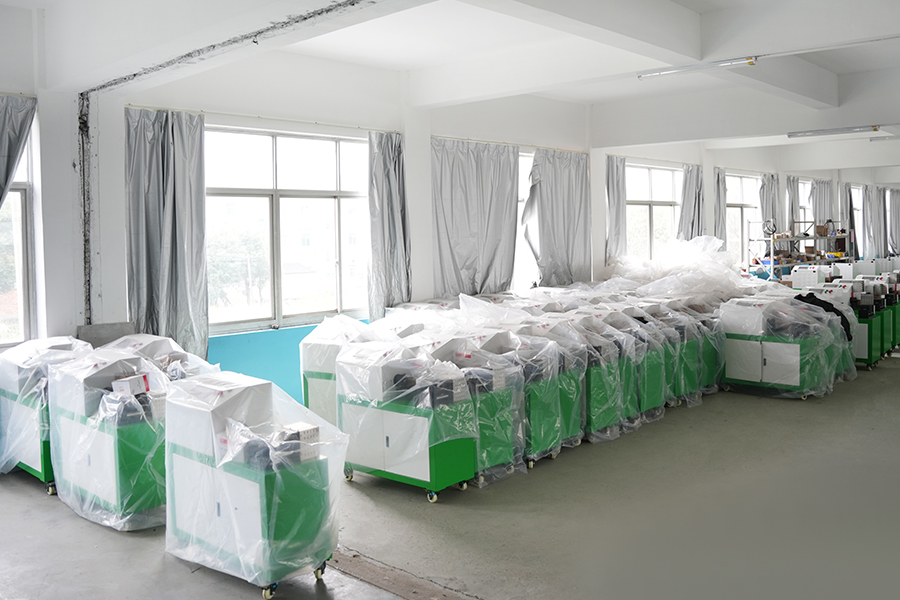
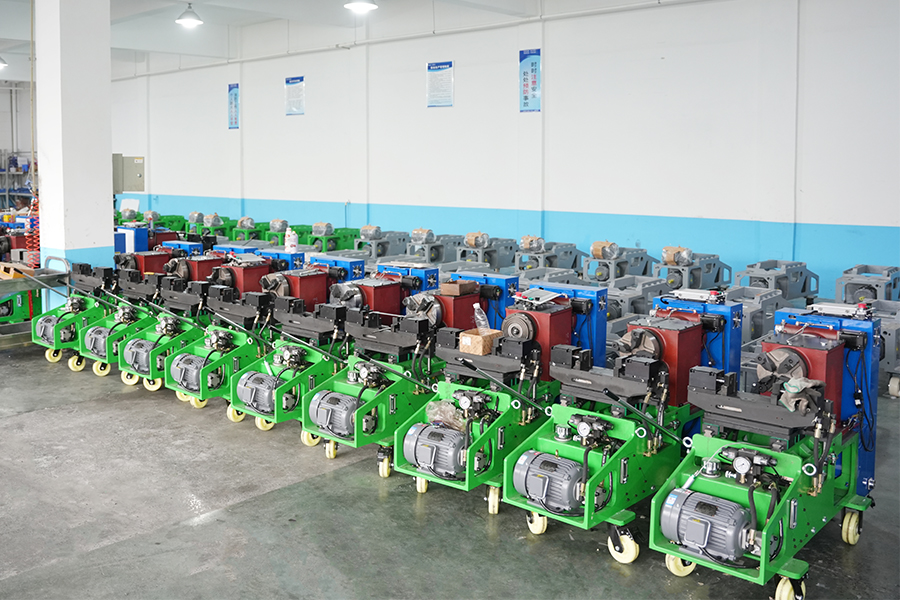
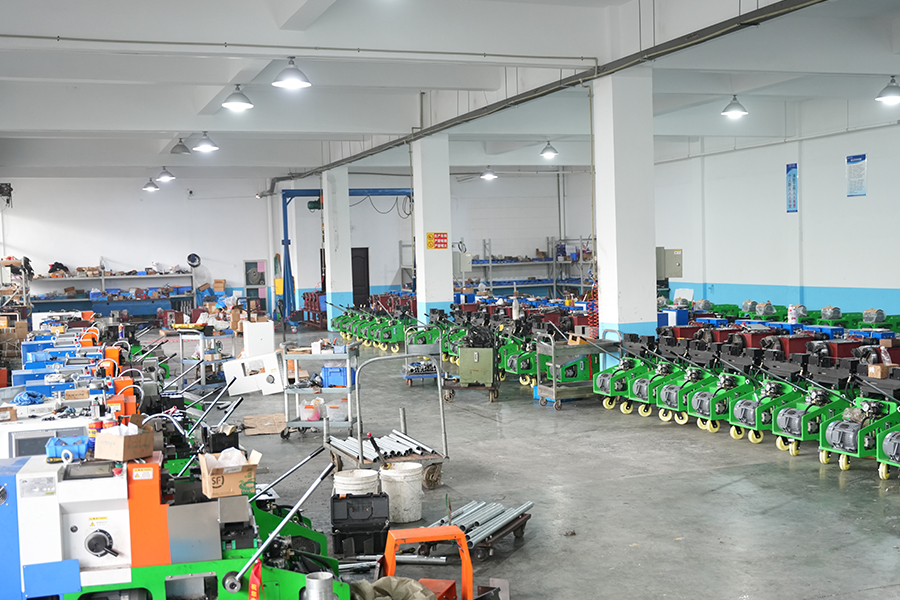
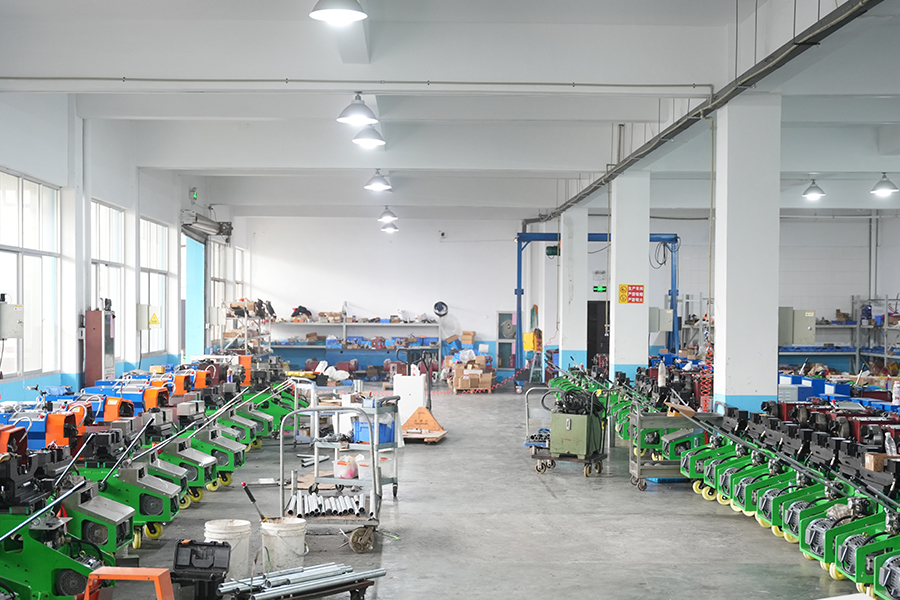
Machines are assembled in our factory in Xiaoshan, Hangzhou and inspected before dispatch. Conformity documentation covering the Machinery Directive and Electromagnetic Compatibility Directive is issued for the equipment range, and patent documentation for the pipe processing mechanisms is available with the shipment.
- Functional check of drive, feed, clamping and overload stop before packing.
- Hole quality verified on sample pipe of the specified material and wall thickness.
- Conformity attestation and product certificate supplied with the order.
- Spare parts list and operating documentation included in the delivery scope.
Information We Use to Configure Your Solution
These project details let us return a machine configuration, tooling list and quotation matched to the work.
- Pipe material, outside diameter and wall thickness for each size on the drawing.
- Hole diameters required and the outlet or coupling type they serve.
- Full pipe size range the machine must cover, from smallest branch to largest main.
- Site supply voltage, frequency and plug type.
- Shift production target in holes, and whether work is shop-based or on site.
- Mobility requirement — bench-mounted, trolley-mounted or carried between floors.
- Documentation, labelling or conformity requirements for the destination market.
- Spare cutter head and consumable quantities to include in the first order.
Installation, Maintenance and Spare Parts
Commissioning is straightforward: the machine needs a stable surface, a supply within the specified voltage, and a clamping fixture matched to the pipe size. Operating and maintenance documentation is supplied with each unit, and training for installation crews and distributor service staff is available.
- Cutter heads and clamping components are replaceable wear items held as spare parts.
- Routine maintenance covers cutter condition, clamping jaw wear, feed mechanism and electrical connections.
- Overload protection settings are checked as part of periodic inspection.
Frequently Asked Questions
What pipe sizes and hole diameters does the fire pipe drilling machine cover?
Our 220V fire pipe drilling machine produces holes from φ16 mm to φ114 mm on pipe from DN15 to DN200. The clamping fixture holds the pipe during cutting, so the same machine handles small branch lines and large mains within that range.
Which pipe materials can be drilled?
Galvanized steel pipe, seamless steel pipe, PVC pipe, carbon steel, stainless steel, aluminium and copper. Cutter head selection and feed pressure are matched to the material and wall thickness during configuration.
Do the holes need deburring after cutting?
No. The cutter produces smooth, burr-free edges that are ready for the coupling or outlet fitting without a secondary finishing operation.
What happens if the cutter meets a hard section of pipe wall?
Built-in overload protection stops the tool automatically. This prevents cutter damage and keeps the operator clear of the work area while the condition is cleared.
Can the machine be used on site as well as in a fabrication shop?
Yes. The machine is built for both prefabrication and site installation. Tell us the mobility requirement with your enquiry and we will confirm the mounting and handling arrangement. The wider Pipe Fabrication & Installation Equipment range covers cutting, threading, tightening and pressure testing for the same projects.
What information is needed for a quotation?
Pipe material, outside diameter and wall thickness, required hole diameters, the full pipe size range, site voltage, production target and any documentation requirements. With those details we specify the machine, tooling and spare parts for the project.
 English
 Español
 عربى